English

Huadong: Established in 1986
Inquiry Us Now
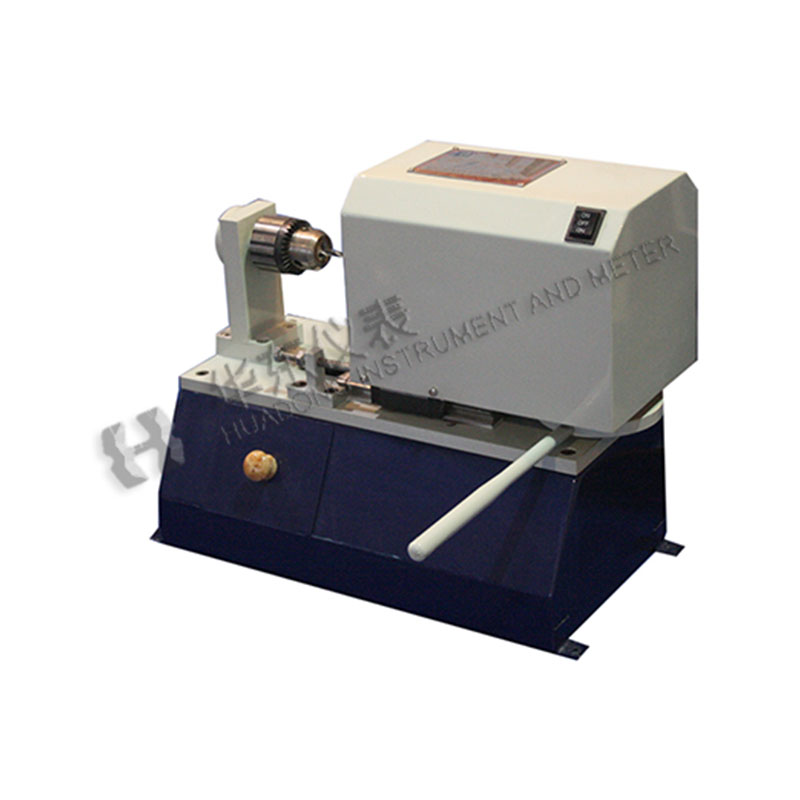
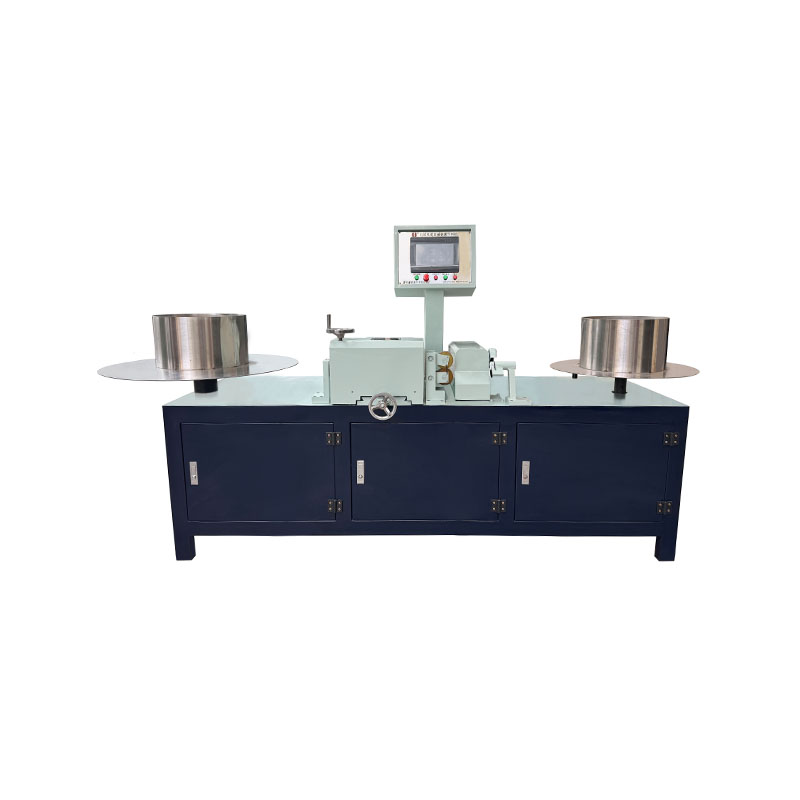
Traditional manual drilling methods are prone to three major flaws: hole eccentricity, accidental penetration of the armored sheath, and inconsistent drilling depth. Uneven residual magnesium oxide insulation powder directly leads to temperature measurement drift in thermocouples and product scrapping; the HYZKJ-01 model structurally eliminates these issues. The equipment features a built-in positioning and limit mechanism that allows the drilling depth to be locked as required, ensuring uniform hole depth across an entire batch of armored cables. This consistency facilitates the standardization of internal powder removal and thermocouple wire length, ensuring uniformity in subsequent thermoelement welding and end-cap processing; it eliminates temperature measurement errors at the source and significantly reduces the rework rate during sensor calibration. Specialized fixtures accommodate armored cables ranging from Φ3mm to Φ10mm; once clamped, the cable is perfectly coaxial with the drill bit, preventing issues such as off-center drilling, scratching of the stainless steel sheath, or wall penetration that would ruin the part. Weighing only 40kg and measuring 500×250×300mm, the unit is compact enough to be placed directly on an assembly line workbench. Unlike manual bench drills—which require the operator to hold the cable, repeatedly measure depth, and clear away powder (resulting in long processing times per unit)—this machine integrates positioning, drilling, and chip removal into a single step. It enables continuous batch processing by a single operator, boosts output within the same timeframe, and is ideally suited for high-volume assembly line production.